Understanding the Importance of Quality Double Ram Blowout Preventers in Industrial Applications
2024-08-10
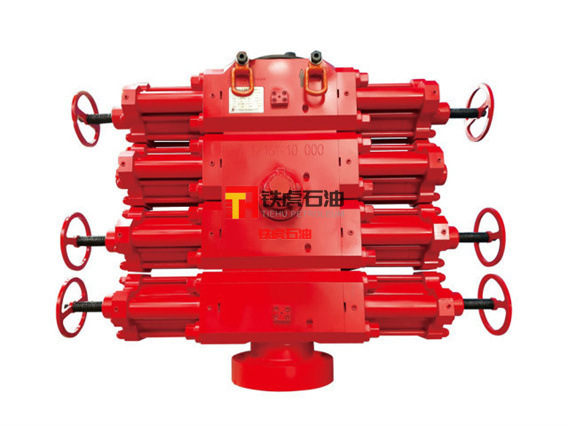
In the realm of industrial equipment, particularly in the valve manufacturing sector, the importance of quality double ram blowout preventers (BOPs) cannot be overstated. These devices are essential for controlling and managing wellbore pressure during drilling operations. A well-designed double ram BOP provides a robust solution to prevent blowouts, which can lead to catastrophic accidents, environmental disasters, and significant financial losses.
Double ram blowout preventers are engineered to seal the wellbore by using two sets of hydraulic rams. This dual sealing capability offers enhanced safety compared to single ram designs, allowing for greater pressure control and reliability. In high-pressure environments—common in oil and gas drilling—this design serves as a critical line of defense against unexpected pressure surges.
One of the primary benefits of using quality double ram BOPs is their ability to provide redundancy. Should one ram fail, the other can still function effectively, maintaining the integrity of the well and protecting personnel and equipment. This redundancy is vital in high-risk environments, where the stakes are particularly high, and operational downtime can lead to substantial costs.
Furthermore, the use of advanced materials and engineering techniques in manufacturing quality double ram blowout preventers enhances their durability and performance. These improvements contribute to longer service life and reduced maintenance needs, ultimately leading to cost savings for operators. When evaluating the effectiveness of a BOP, the quality of the materials used—such as high-strength alloys and corrosion-resistant coatings—plays a significant role in the device’s longevity and reliability.
Moreover, compliance with industry standards and regulations is paramount in the production of double ram blowout preventers. Quality BOPs are designed to meet the stringent requirements set forth by regulatory bodies, ensuring that they can withstand extreme conditions and function effectively when needed. This compliance not only enhances safety but also builds trust with clients and stakeholders, reinforcing the reputation of the manufacturer.
In conclusion, the significance of quality double ram blowout preventers in the industrial equipment sector, especially within valve manufacturing, is profound. Their ability to provide safety, reliability, and efficiency makes them indispensable in high-pressure operations. By investing in high-quality BOPs, companies can safeguard their operations, protect their workforce, and reduce the risk of costly blowouts. Understanding the critical role these devices play can help professionals in the industry make informed decisions that prioritize safety and operational efficiency.
Related News
Contact Us
Mailbox:
tiehu@tiehupetro.com
Telephone:
86-317-2616808
Address:
Yanling Industrial Zone, Renqiu City, Cangzhou City, Hebei Province, China
Hebei New Tiehu Petroleum Machinery Co., Ltd.
Sales Line: +86-317-7651717
Telephone:+86-317-2616808 -8009
Mailbox:tiehu@tiehupetro.com
Address: Yanling Industrial Zone, Renqiu City, Cangzhou City, Hebei Province, China


Focus on us
Follow us